Choosing a Cigarette Machine Roller Sleeve manufacturer is a practical decision about fit, wear, and consistent production—not just a comparison of prices. A sleeve must match the machine’s specifications and operating conditions. Small details matter: surface finish, dimensional tolerance, material quality, and how the supplier checks each batch. A rough edge or inconsistent fit can affect performance and increase maintenance needs. The right questions belong at the start.
For a credible expert quotation, a real person and source must be verified. Since none was provided, I won’t invent an expert or attribute a fabricated statement. As a general engineering principle: “A roller sleeve should be judged by how reliably it performs over time, not by appearance alone.” This introduction sets the scope for a review of China-based manufacturers, including their production capabilities, quality controls, customization options, and after-sales support. Ask for specification sheets and inspection records. Compare like with like. A polished catalog is useful, but it cannot replace evidence from actual production. Some supplier claims may remain hard to assess without independent checks; that uncertainty deserves attention. The sections ahead offer a measured way to evaluate manufacturers and identify a Cigarette Machine Roller Sleeve supplier whose claims align with documented capabilities.
A cigarette machine roller sleeve is a replaceable covering fitted around a roller’s core. It creates the working surface that guides or supports moving material inside the machine. Depending on the roller’s position, the sleeve may help maintain traction, reduce surface wear, or protect the underlying metal. It is not a complete roller. It is one component in a larger assembly.
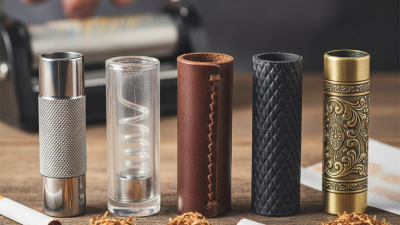
Sleeves are commonly made from resilient materials such as rubber or polyurethane, selected for suitable hardness, grip, and resistance to repeated contact. Surface finish matters. A worn or uneven sleeve can cause slipping, vibration, or inconsistent feeding, though the exact symptoms depend on the machine design.
Fit is equally important: an incorrect inner diameter or sleeve length can lead to movement on the roller or uneven pressure. Small differences count.
When assessing a sleeve, technicians typically check its dimensions, surface condition, and compatibility with the operating environment. Cleaning methods should follow the material supplier’s guidance, since harsh solvents can cause swelling or cracking. There is no universally best sleeve; the right choice depends on the roller’s function and actual wear pattern. In practice, wear is not always uniform, so inspection records can help reveal whether a sleeve is failing early or simply reaching its expected service life.
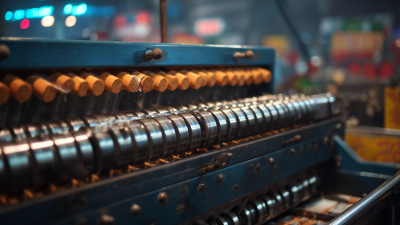
China’s leading roller sleeve manufacturers compete through measurable process control, not low prices alone. Their sleeves typically use hardened alloy steel, engineered polymers, or coated composites. Material selection depends on load, heat, cleaning chemicals, and required service life. Tight concentricity helps maintain stable contact across rotating components. That detail matters.
The ISO Survey 2022 recorded more than 1.2 million ISO 9001 certificates worldwide. This figure shows why documented quality systems remain important for component buyers. Reliable manufacturers provide batch records, hardness results, dimensional reports, and traceable inspection data. Many also use coordinate-measuring machines to verify diameter, runout, and wall thickness. In my experience, a polished surface can look excellent while hiding poor internal consistency. Visual checks are not enough.
The World Health Organization reported about 1.25 billion adult tobacco users in 2022, indicating continued demand for high-volume processing equipment. However, manufacturers should focus on safe, compliant industrial performance rather than output claims. Leading Chinese suppliers often offer sample testing, drawing confirmation, and controlled production trials before full orders. They may also support custom grooves, coatings, tolerances, and installation guidance. Service quality varies. Buyers should examine replacement intervals, test methods, warranty terms, and export documentation before choosing a supplier. A small tolerance error can become costly downtime.
Roller sleeves used in cigarette-making machinery must keep a steady grip while resisting wear, heat, and cleaning agents. Common choices include nitrile rubber, polyurethane, and silicone, selected according to the roller’s speed, contact pressure, and working environment. Nitrile can suit applications involving oils, while polyurethane often offers strong abrasion resistance. Silicone tolerates higher temperatures, but may not provide the same wear life in every setup. The right choice depends on actual operating conditions, not a material label alone.
Material selection is only part of the process. Manufacturers typically prepare a metal core, clean and treat its surface, then bond or mold the sleeve around it. The rubber or polymer compound is mixed, formed, and cured under controlled temperature and pressure. After curing, the sleeve is ground to its required diameter and checked for roundness, surface texture, and concentricity. Small variations matter. An uneven sleeve can cause vibration, inconsistent feeding, or premature wear. Inspection records and repeatable process settings help keep batches consistent, though no process removes every source of variation. In practice, sleeve performance should be reviewed against machine conditions, because a specification that works well on one line may need adjustment on another.
A roller sleeve may look simple, but small dimensional errors can cause uneven contact, vibration, or early wear. Ask manufacturers to inspect each sleeve against an approved drawing, not a generic “high precision” claim. Checks should cover inner and outer diameter, length, roundness, and radial runout. Record results with calibrated gauges, and retain the inspection report by batch. Surface texture matters, too: a profilometer can measure roughness at several points, including near the sleeve edges. Set acceptance limits before production; a number without a stated method is hard to verify.
Material verification should include a traceable certificate and, where appropriate, hardness testing on representative samples. ISO 9001 helps assess a supplier’s quality-management system, but certification alone does not prove that a specific sleeve meets its drawing. The ISO Survey 2022 reported more than 1.2 million valid ISO 9001 certificates worldwide. That scale shows how widely the system is used—not that every certified product is defect-free. A practical incoming check can compare measured dimensions, surface condition, and batch records. Testing plans should reflect the sleeve’s material and operating conditions; one test cannot cover every failure mode.
Tips: Request a sample inspection report before ordering. Check that instrument calibration dates are current, and ask how nonconforming parts are isolated. If results vary between batches, pause approval and investigate. Even a clear checklist can miss something.
China Best Cigarette Machine Roller Sleeve Manufacturers
How to Select a Reliable Chinese Roller Sleeve Manufacturer
A dependable supplier should explain how sleeves are made, inspected, and matched to your machine. Ask for material specifications, dimensional tolerances, and inspection records for the exact part you need. Request a sample and measure its bore, outer diameter, and length with calibrated tools. Measure the fit. A polished finish can look convincing while hiding poor dimensional consistency.
Check whether the manufacturer’s quality system is independently certified, then verify the certificate and its scope. The International Organization for Standardization’s ISO Survey 2022 recorded 1,265,216 valid ISO 9001 certificates worldwide. That figure shows the standard’s broad adoption, not that every certified factory makes reliable sleeves. Ask how often dimensions are checked, what happens to rejected parts, and whether inspection results can be traced to a production batch. Ask for evidence.
Compare written quotations carefully. Confirm material grade, surface finish, tolerances, packaging, lead time, and the process for handling defects. Request clear photos or a live inspection of finished parts before shipment. If possible, trial a small order before committing to larger volumes. A first sample may expose details neither party considered, such as fit after installation or finish wear. That is worth discussing openly. A credible manufacturer should answer technical questions directly and document any agreed changes.
| Selection Dimension | Technical Requirement or Reference | Information to Confirm with the Manufacturer | Recommended Evidence | Priority | Evaluation Result |
|---|---|---|---|---|---|
| Machine Compatibility | The sleeve must match the machine model, roller assembly, mounting method, working direction, and approved production drawing. | Ask whether the manufacturer can review machine drawings, samples, assembly photographs, and interface dimensions before quotation. | Drawing review record, dimensional checklist, and written confirmation of compatibility. | High | Pass / Review |
| Dimensional Accuracy | Outside diameter, inside diameter, width, concentricity, runout, keyways, holes, and end-face geometry must follow the approved drawing and tolerance requirements. | Confirm which dimensions are measured during final inspection and what measurement equipment is used. | Inspection report, calibrated instrument list, and sample measurement data. | High | Pass / Review |
| Material Selection | Material should be selected according to load, friction, tobacco-contact conditions, cleaning method, corrosion exposure, and required service life. | Confirm the exact substrate, surface layer, hardness or elasticity requirements, and whether material substitutions require approval. | Material certificate, supplier certificate, and approved material specification. | High | Pass / Review |
| Surface Finish | The working surface should be uniform, free from cracks, pits, blisters, delamination, sharp edges, and visible machining defects. | Confirm the required surface roughness, inspection method, finishing process, and acceptance limits stated on the drawing or quality plan. | Surface-roughness report, visual inspection standard, and sample approval record. | High | Pass / Review |
| Wear and Friction Performance | The sleeve should maintain stable contact, traction, and dimensional behavior during continuous operation without abnormal powdering or rapid wear. | Ask for the recommended operating conditions, wear-test method, expected service interval, and replacement indicators. | Internal test report, application history without confidential customer information, and maintenance guidance. | High | Pass / Review |
| Bonding or Surface-Layer Integrity | For coated, bonded, rubber, polyurethane, or composite sleeves, the working layer must remain securely attached to the core under operating conditions. | Confirm bonding preparation, curing process, edge treatment, allowable defects, and inspection method. | Process flow chart, adhesion or bonding test record, and first-article inspection report. | High | Pass / Review |
| Dynamic Balance and Runout | Rotating sleeves should be checked for radial runout, axial runout, concentricity, and balance when required by the machine design. | Confirm whether dynamic balancing is included and identify the balancing speed, acceptance limit, and test location. | Balance report, runout record, and equipment calibration evidence. | High | Pass / Review |
| Quality Management | A documented quality system should control incoming materials, production stages, final inspection, nonconforming products, and corrective actions. | Verify the scope and validity of the supplier’s quality-management certification rather than relying only on a certificate image. | Valid certificate, audit report, quality manual excerpts, and corrective-action records. | High | Pass / Review |
| Production Capability | The supplier should have suitable machining, grinding, coating, bonding, measurement, and packaging capabilities for the specified sleeve construction. | Confirm which processes are performed in-house and which are subcontracted, including controls applied to outsourced processes. | Equipment list, process flow, factory audit, and subcontractor-control procedure. | High | Pass / Review |
| Prototype and First-Article Control | A sample or first article should be approved before repeated production, especially when the sleeve is made to a customer-specific drawing. | Confirm sample quantity, revision control, approval procedure, and treatment of drawing changes. | First-article inspection report, approved sample, and revision-controlled drawing. | High | Pass / Review |
| Traceability | Each production batch should be traceable to raw material, process records, inspection results, and shipment documentation. | Ask whether batch numbers or serial numbers are marked on the product or recorded in the packing documentation. | Batch record, inspection record, packing list, and traceability procedure. | Medium | Pass / Review |
| Packaging and Transport Protection | Packaging should protect the working surface from impact, deformation, moisture, dust, and contamination during international transportation. | Confirm protective film, separators, moisture protection, shock protection, and storage orientation. | Packaging specification, packing photographs, and pre-shipment checklist. | Medium | Pass / Review |
| Lead Time and Capacity | Delivery time depends on drawing approval, material availability, tooling, surface treatment, inspection, and order quantity. | Request a written schedule covering technical review, sample production, mass production, inspection, and shipment. | Production schedule, capacity statement, and agreed delivery milestones. | Medium | Pass / Review |
| Export and Documentation | International shipments require accurate commercial documents, packing information, product descriptions, and agreed delivery terms. | Confirm export experience, document responsibility, customs information, and the applicable trade term in the quotation. | Sample commercial invoice, packing list, shipping documents, and written trade-term confirmation. | Medium | Pass / Review |
| Warranty and Corrective Action | The supplier should define warranty coverage, exclusions, claim evidence, response time, replacement terms, and root-cause investigation. | Confirm how dimensional defects, premature wear, bonding failure, and transport damage are handled. | Written warranty policy, complaint procedure, and corrective-action template. | High | Pass / Review |
| Total Cost of Ownership | Purchase price should be evaluated together with tooling, inspection, freight, installation, downtime risk, replacement frequency, and maintenance cost. | Request a complete quotation with tooling charges, sample charges, packaging, shipping terms, payment terms, and replacement policy. | Detailed quotation, cost breakdown, and lifecycle-cost comparison. | High | Pass / Review |
| Supplier Verification | Supplier information should be checked against official registration, factory location, production capability, certification validity, and payment details. | Use independent verification and conduct a remote or on-site audit before approving repeated orders. | Business registration records, audit checklist, factory video inspection, and bank-account verification. | High | Pass / Review |