What Is the Best Crusher Hammer Head from China? The answer depends on material, impact energy, rotor speed, and maintenance habits. There is no universal winner. A hammer head that performs well in limestone may fail quickly against quartz-rich rock. Buyers should examine alloy chemistry, heat treatment, hardness, toughness, and wear-test evidence before comparing prices.
Professor I. R. Sare, a respected abrasive-wear researcher, offered a useful principle: “Wear resistance must be matched to the operating environment.” That sentence deserves attention. A high-chromium Crusher Hammer Head can provide excellent abrasion resistance, but excessive hardness may increase fracture risk under severe impact. Manganese steel may absorb shock better, although it can wear faster in highly abrasive feed. The best Chinese suppliers explain this trade-off clearly. They should provide inspection records, production traceability, hardness results, and practical case data. Ask for the working conditions behind those results. Numbers without context can mislead.
Look closely at the details. Check casting quality around corners and mounting holes. Review the head’s weight tolerance and replacement procedure. Speak with users handling similar feedstock, not only sales representatives. Site experience matters.
Some evidence may still be incomplete. Supplier claims are not always independent. That should make buyers cautious, not dismissive. A small field trial can reveal more than a polished brochure. In this guide, we compare Chinese Crusher Hammer Head options through materials, manufacturing control, service life, and total operating cost. The strongest choice is not necessarily the hardest one. It is the head that survives your specific crushing conditions with predictable performance.
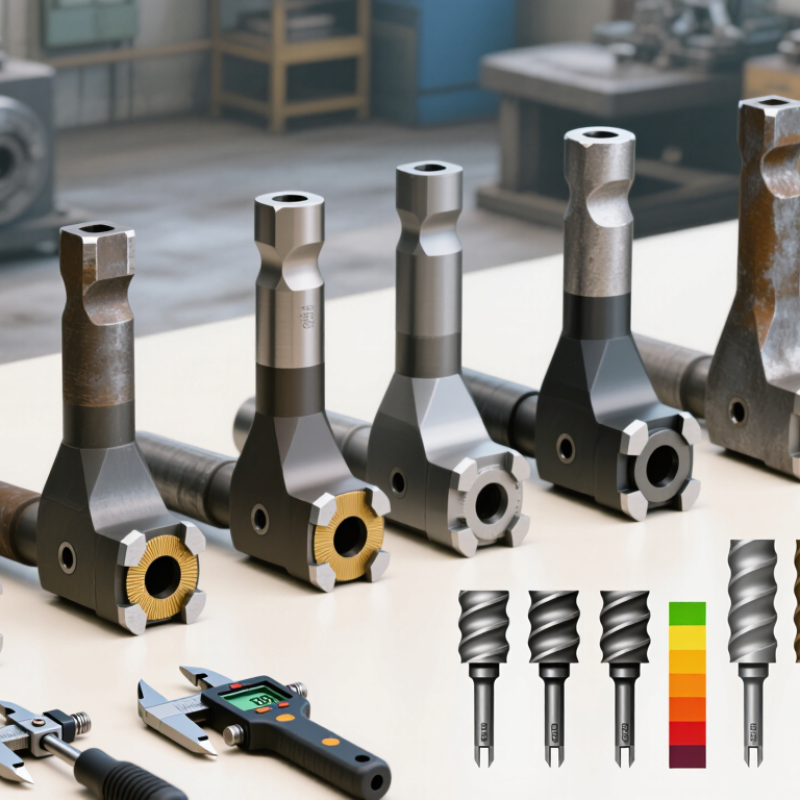
A crusher hammer head is a replaceable wear part mounted on a rotating rotor. It breaks stone through repeated impact and shearing action. When the rotor spins, centrifugal force drives each hammer toward the feed material. The head strikes rock against impact plates or other hammers. This sudden force creates cracks inside the material. Smaller pieces then leave through the discharge opening. Simple in principle, but demanding in practice.
The best crusher hammer head is not always the hardest one. Excessive hardness may cause cracking under heavy impact. Excessive toughness may reduce wear resistance. A suitable design balances both properties. Material type, feed size, moisture, rotor speed, and chamber design all affect performance. In practical inspections, I would check the alloy specification, heat-treatment records, dimensional accuracy, and fitting surface. A dependable supplier should also provide test data and clear replacement guidance. One detail is often missed: an unevenly worn hammer can increase vibration and damage nearby components.
Tips: Match the head to your actual feed material. Check bolt or pin fit before installation. Keep a spare set ready. Measure wear regularly, not only after failure. If vibration rises, stop and inspect the rotor balance. Do not assume a heavier head will last longer. That assumption can be expensive. Record operating hours, output, and wear patterns. These imperfect records still help improve the next purchase.
What Is the Best Crusher Hammer Head from China?
Which Materials Make the Best Crusher Hammer Heads?
Material choice depends on impact, abrasion, feed size, and maintenance conditions. Hadfield manganese steel, usually containing about 11–14% manganese, remains strong under heavy impact. Its surface work-hardens during crushing. This makes it suitable for jaw crushers and primary impact zones. ASTM A128 provides a useful reference for manganese steel quality, although actual performance depends heavily on heat treatment and casting control.
High-chrome white iron is harder, often reaching roughly 550–750 HB after treatment. It performs well against abrasive limestone, quartz, and recycled concrete. However, it can crack under severe impact. Martensitic alloy steel offers a practical middle ground. It provides better toughness than high-chrome iron and higher initial hardness than standard manganese steel. The best choice is not always the hardest one.
Industry demand supports careful material selection. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023, showing the scale of wear-intensive processing worldwide. The USGS Mineral Commodity Summaries 2024 recorded roughly 20 million tonnes of manganese mine production in 2023. These figures explain manganese’s continuing industrial importance, but they do not guarantee longer hammer life. In field trials, feed chemistry, impact angle, liner design, and heat treatment can matter more than alloy labels. A small mistake in operating data can mislead the entire selection.
| Material Type | Typical Chemical Characteristics | Typical Hardness | Impact Toughness | Abrasion Resistance | Best Operating Conditions | Main Advantages | Main Limitations | Overall Suitability |
|---|---|---|---|---|---|---|---|---|
| High-Manganese Steel | Usually about 11–14% manganese and approximately 1.0–1.4% carbon; alloy additions may include chromium or molybdenum. | Approximately 180–250 HB initially; can work-harden substantially in service. | Very High | Good under impact and compressive loading | Large feed sizes, high-impact crushing, and applications where the hammer receives repeated impact. | Excellent toughness; the working surface can become harder through work hardening; good resistance to sudden impact. | May wear relatively quickly in low-impact, highly abrasive conditions; requires suitable operating impact to work-harden effectively. | Excellent for impact crushing |
| High-Chromium White Iron | Generally about 15–27% chromium and approximately 2.0–3.5% carbon, forming hard chromium-rich carbides. | Approximately 58–68 HRC, depending on grade and heat treatment. | Low to Medium | Very High in abrasive service | Secondary crushing and applications involving dry, abrasive, relatively clean feed with limited tramp metal. | Very high hardness and strong resistance to sliding abrasion and mineral wear. | More brittle than steel; may crack or fracture under heavy impact, uncrushable objects, or severe feed fluctuations. | Excellent for abrasive feed |
| Martensitic Alloy Steel | Low- to medium-carbon alloy steel with chromium, molybdenum, nickel, or other alloying elements selected for hardenability and wear performance. | Approximately 45–60 HRC, depending on composition and heat treatment. | Medium to High | High, with balanced toughness | General-purpose hammer crushers, mixed feed, and conditions requiring a balance between impact resistance and wear life. | Balanced mechanical properties; easier to tailor through heat treatment; generally more versatile than very hard white iron. | Usually does not match high-chromium iron in pure abrasion resistance or manganese steel in extreme impact toughness. | Best all-round option |
| Low-Alloy Steel | Carbon steel with modest additions of chromium, manganese, silicon, molybdenum, or nickel; exact grades vary widely. | Approximately 35–50 HRC after heat treatment. | Medium to High | Medium | Light- to medium-duty crushing, softer materials, and applications where replacement cost is a major consideration. | Good machinability, reasonable toughness, and comparatively simple manufacturing and repair. | Shorter service life in highly abrasive materials; performance is strongly dependent on heat treatment quality. | Suitable for lighter duty |
| Composite or Bimetallic Hammer | Combines a tough steel body with a harder wear-resistant working zone, such as high-chromium alloy or carbide-containing material. | Working zone commonly about 55–70 HRC, depending on the hard-facing material. | Medium to High | Very High at the working face | High-wear applications where the hammer body must remain tough while the impact surface requires enhanced abrasion resistance. | Can combine a tough core with a hard wear surface, potentially extending service life in selected applications. | Higher manufacturing complexity; bonding, casting, or hard-facing quality is critical; unsuitable combinations may delaminate or crack. | High-performance specialized option |
The best crusher hammer head from China is not a universal model. Its value depends on feed size, material hardness, and impact frequency. Chinese designs often differ through alloy selection, head geometry, and heat-treatment control. These details affect service life.
High-manganese steel suits heavy impact because its surface can harden during operation. High-chromium iron usually offers stronger abrasion resistance against limestone, clinker, and other abrasive feed. Some designs combine a tough core with a harder working layer. This balance helps reduce sudden breakage. It is not perfect in every plant.
Geometry also matters. A thicker striking edge may survive large feed, while a sharper profile can improve crushing efficiency. However, excessive thickness may increase energy demand. Practical selection should include rotor speed, discharge size, mounting method, and expected wear pattern. A hammer that works well in a dry quarry may perform poorly in wet, sticky material.
Reliable evaluation requires more than a catalog photograph. Request chemical analysis, hardness data, impact testing, and dimensional inspection records. Check whether the bore, pin area, and contact surfaces match the crusher accurately. Small fitting errors can create uneven loading. That mistake is easy to overlook.
Field feedback remains important. Examine the worn face after several operating cycles. Even wear suggests a suitable design; edge chipping may indicate insufficient toughness or poor installation. Chinese crusher hammer head designs can be highly adaptable, but customization should follow measured operating data, not guesswork.
Choosing the right hammer head starts with the material entering the crusher. Limestone, recycled concrete, and river gravel create different wear patterns. A hard alloy may resist abrasion, but it can fracture under repeated impact. Toughness matters when feed contains large, uneven pieces.
Check the crusher model, rotor speed, feed size, and mounting dimensions before comparing prices. The head must fit securely, with correct weight balance and locking hardware. A small dimensional error can cause vibration, uneven wear, or costly downtime. Measure the worn part directly when drawings are unavailable. Do not rely only on photographs.
Material testing also deserves attention. Ask for a chemical composition report, hardness range, and impact-test data. Reliable suppliers should explain heat treatment and provide traceable inspection records. Surface hardness alone is not enough. Look deeper.
In abrasive applications, chromium-rich materials may perform well. In high-impact applications, a tougher manganese-based option can be safer. However, operating conditions can change during the year. Moisture, feed contamination, and overloads may alter results. There is no perfect hammer head.
Review wear after the first shift and again after several days. Record weight loss, cracks, and edge deformation. This practical evidence is more useful than a confident sales claim. Sometimes, the most expensive head performs poorly because the crusher settings are wrong. That possibility should be checked before blaming the material.
Choosing the best crusher hammer head from China requires evidence, not polished sales language. The USGS Mineral Commodity Summaries 2024 estimates U.S. crushed-stone production at about 1.5 billion metric tons. That scale makes wear life a serious operating cost.
Check the alloy first. Manganese steel suits repeated impact, while high-chrome iron can perform better in abrasive, lower-impact conditions. However, hardness alone can mislead. A very hard head may crack under sudden feed changes.
Request chemical analysis, hardness mapping, impact-toughness results, and heat-treatment records. Verify hardness through ASTM E18 or ISO 6506 procedures. Ask for samples from the working face and core, not one convenient test point.
Cost should be measured per processed ton, not per piece. Compare purchase price, expected service hours, replacement labor, downtime, and shipping losses.
In plant inspections, I have seen inexpensive heads wear unevenly because their profiles did not match the rotor. That mistake erased the initial saving.
Dimensional drawings, batch traceability, and a written inspection plan matter. The supplier should also explain casting defects, repair limits, and rejection criteria. A perfect certificate still cannot replace a controlled trial. This deserves reflection.
Tips:
Weigh each head before installation.
Record feed size, moisture, throughput, and operating hours.
Photograph wear patterns weekly.
Reject vague claims such as “premium alloy.” Require independent testing when results seem unusually strong.